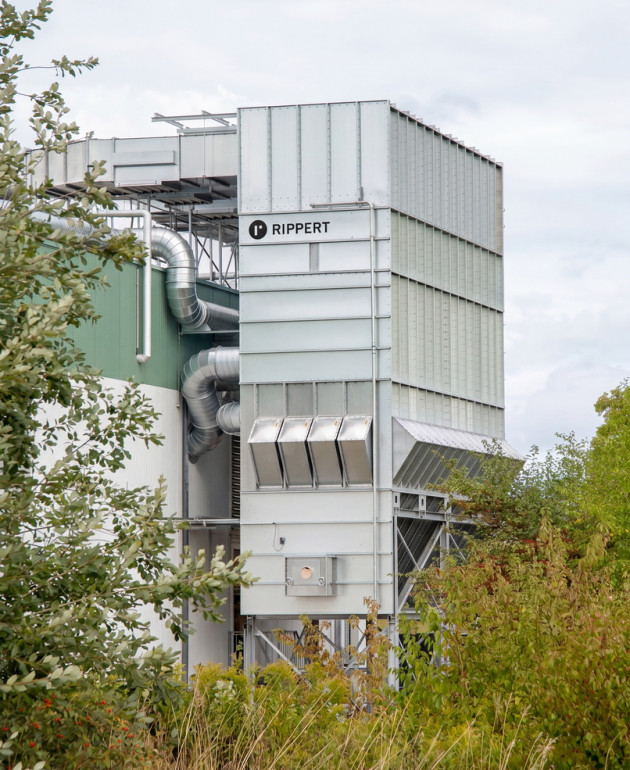
RIPPERT-News Becker relies on powered extraction
To ensure that high standards of quality and sustainability are maintained in production too, Becker relies on efficient extraction and filtration technology. As part of a comprehensive modernisation programme, the production facility was fitted with an energy-efficient extraction system.
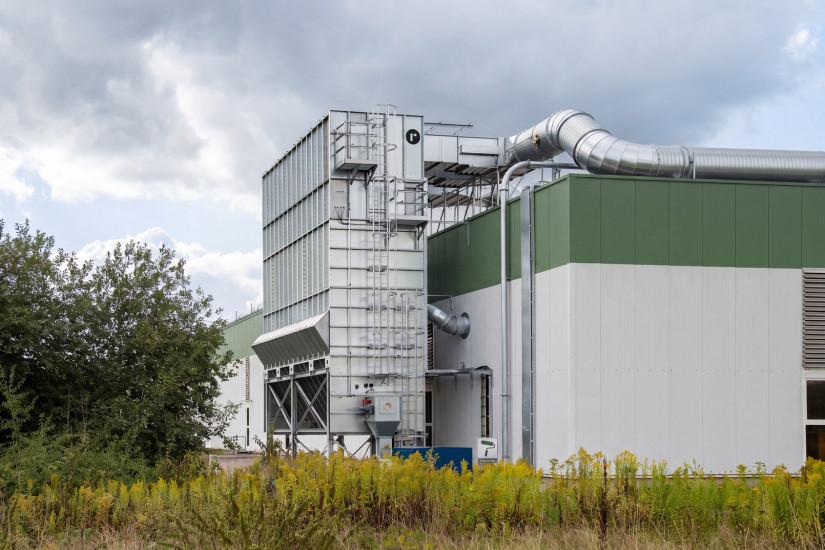
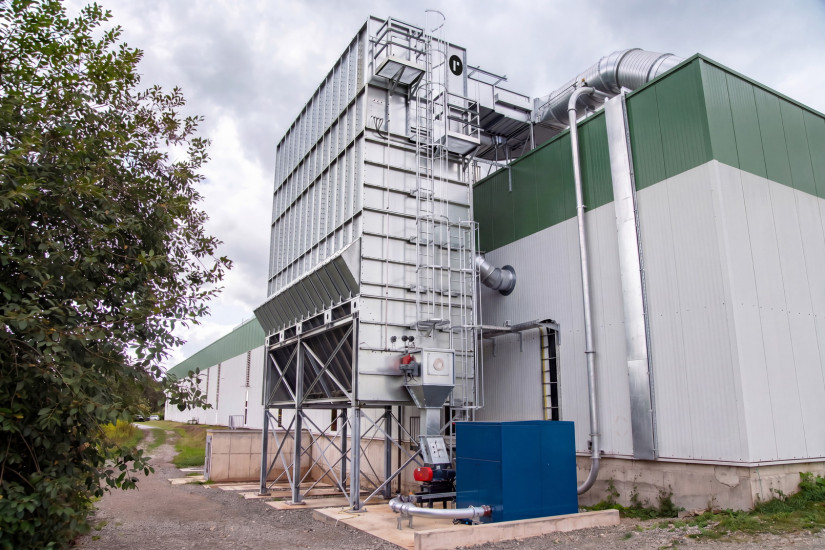
Becker: The Art of Shaping Fritz Becker GmbH & Co. KG is a long-established, medium-sized company specialising in the shaping of wood and non-woven fabrics. With over 700 employees across three sites, the company produces high-quality mass-produced goods which, through close collaboration with designers and customers, continually set new standards. Research, innovation and a spirit of partnership have characterised the company’s culture for four generations. Sustainable production through efficient extraction technology The new system not only ensures a clean working environment but also makes a significant contribution to reducing energy consumption through intelligent control and energy-optimised fan technology. Through the use of variable-frequency drives and demand-based air volume control, the extraction capacity is precisely adapted to actual production requirements. This enables considerable savings to be realised in terms of electricity and heat. Modernisation in three phases The project is being implemented in three clearly defined phases. The first phase was successfully completed in the summer of 2025. The second phase will follow this year, whilst the third phase is planned for the summer of 2027. As part of this modernisation, RIPPERT is replacing a total of four older filter systems, whose fans are significantly less efficient. Once all measures have been completed, the new extraction system will handle an air volume of around 280,000 m³/h – thereby significantly increasing both the efficiency and sustainability of production at Becker. Efficient material transport via high-pressure conveying A key feature of the new extraction system is the transport of the extracted material. Instead of relying on conventional fan technology, the material is conveyed via high-pressure conveying. The separated swarf and dust are conveyed from the filter system to a silo approximately 200 m away. The advantage of this technology is that the volume flow rates are significantly lower than those of ‘conventional fans’. Instead, higher pressure is available, meaning that even large quantities of material can be transported safely and efficiently over long distances. This solution combines maximum operational reliability with optimised energy use. From planning to implementation – a team effort by RIPPERT The project was developed and costed by the sales department. Following a successful agreement with Becker, the responsible project manager took charge of the planning and implementation of the system. Through this close collaboration – encompassing technical design, commercial coordination and professional project management – a bespoke solution was created that is perfectly tailored to Becker’s production processes. The exceptional quality of this collaboration is particularly worth noting: Collaboration based on partnership The close coordination between Becker and RIPPERT enabled the extraction system to be seamlessly integrated into the existing production processes. In addition to significant energy savings, the solution offers high operational reliability, low maintenance requirements and a sustainable improvement in working conditions. Following the full implementation of the three construction phases, Becker now has a state-of-the-art extraction system with a total capacity of 280,000 m³/h. Four older filter systems with inefficient fans will be completely replaced by then. The new solution features energy-optimised fan technology, the use of variable-speed drives, demand-based airflow control and the use of high-pressure conveyance for the 200-metre-long material transport to the silo.
With this investment, Becker is sending a clear signal in favour of future-oriented, resource-efficient production – whilst at the same time underlining its commitment to combining technological excellence with environmental responsibility.
